When I first heard about DTF printing, I was skeptical. After fifteen years of pulling squeegees and wrestling with plastisol, the idea of a digital transfer that could handle any fabric felt too good to be true. But after running thousands of prints through my own shop, I can tell you this: DTF is not a fad. It is a legit tool that has changed how I quote small orders and handle complex artwork. If you are a screen printer, a print-on-demand seller, or someone who just wants to make custom shirts without a garage full of equipment, this guide is for you. I will walk you through what DTF actually is, where it shines, where it fails, and how to decide if it deserves a spot in your workflow.
What Exactly Is DTF Printing?
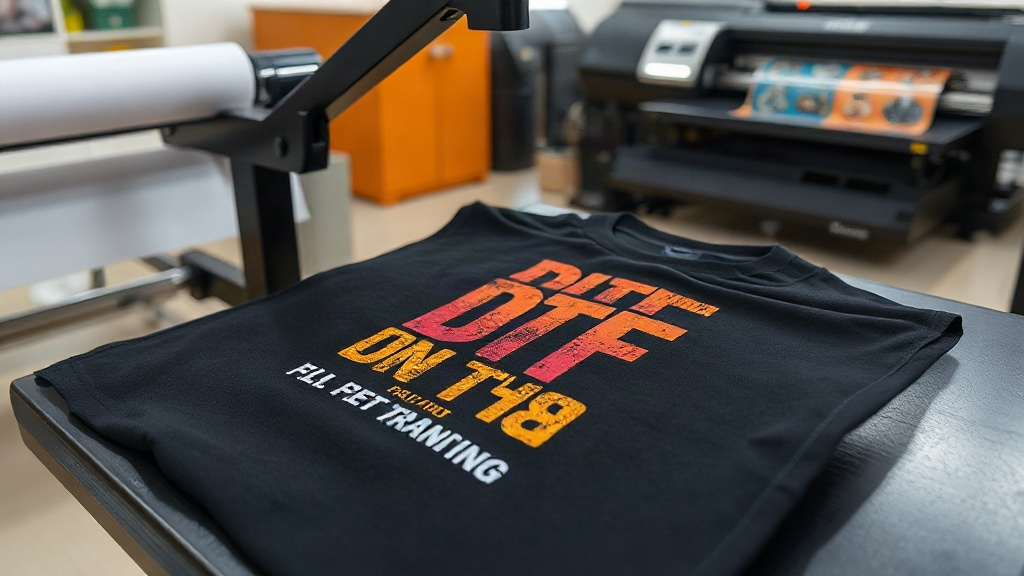
DTF stands for Direct to Film. The process starts with a digital printer that lays down a layer of white ink, followed by CMYK colors, onto a special PET film. While the ink is still wet, a fine layer of hot-melt adhesive powder is applied. After shaking off the excess, the film is cured in an oven or with a heat press. The result is a flexible, stretchy transfer that you can store indefinitely and apply later with a heat press. Unlike DTG, which prints directly onto the garment, DTF transfers can be applied to almost any fabric: cotton, polyester, blends, even nylon and leather. That versatility is the main reason it has taken off. You are not limited by fiber content or color. Black shirts? No problem. Polyester jerseys? They work fine. This alone makes DTF a powerful complement to screen printing, especially for small runs and sample-making.
How DTF Compares to Screen Printing and DTG
Let us cut through the marketing hype. Each method has a sweet spot. Screen printing still wins for large orders of simple designs. The per-unit cost drops dramatically once you pass a few dozen pieces, and the ink is incredibly durable. DTG is great for 100% cotton shirts with photographic designs, but it struggles on dark colors and synthetics. DTF sits in the middle. It handles small batches efficiently, requires no setup or screens, and works on virtually any fabric. The trade-off is a slightly higher cost per print than screen printing at high volumes, and a hand feel that is a bit thicker than a well-printed plastisol. But for orders under 50 pieces, DTF often beats screen printing on both time and money. I have run side-by-side tests, and for a 24-piece order with six colors, DTF saved me about two hours of setup and cleanup. That is time I can spend on marketing or taking on more jobs.
Cost Breakdown: What You Will Actually Spend
Let us talk numbers. A decent DTF printer setup starts around $3,000 for a converted Epson or a dedicated Chinese model. Then you need a shaker or powder applicator, a curing oven, and a heat press. That can easily push your initial investment to $8,000 or more. But if you already have a heat press for screen printing, you are halfway there. The consumables are where the ongoing costs live. A 100-meter roll of film costs $50 to $80. Ink is around $100 per liter set, and powder is about $30 per kilogram. On average, a 10-inch by 12-inch DTF transfer costs me roughly $1.50 to $2.50 in materials, depending on ink coverage. Compare that to screen printing, where a similar size print on a dark shirt might cost $0.80 in ink but requires a $20 screen and 30 minutes of setup. For a one-off, DTF is a no-brainer. For 500 pieces, screen printing still wins. The key is to know your break-even point. For me, it is around 36 pieces for a multi-color design. Your mileage will vary based on your labor rate and overhead.
Where DTF Shines and Where It Falls Short
I have used DTF for a wide range of jobs. Here is what I have learned:
- Pros: No color limits, no screens, no weeding. You can print full-color photographic images. Works on dark and light fabrics, cotton and polyester. Transfers can be stored for months. Great for personalization and small batches.
- Cons: The hand feel is noticeable, especially on large solid areas. Durability is good but not quite as bulletproof as screen printing if you wash with hot water and harsh detergent. The process requires careful temperature and pressure control, or the transfer will peel. And the equipment needs regular maintenance to avoid clogged printheads.
One more thing: DTF transfers can look slightly glossy. If you want a matte finish, you need to adjust your powder or use a matte film. It is a small detail, but for premium brands, it matters.
Durability: How Long Does a DTF Print Last?
I have washed DTF-printed shirts over 50 times in a standard home washer and dryer. The prints held up well with minimal fading or cracking. The key is to wash inside out in cold water and tumble dry low. Avoid ironing directly on the print. If you follow those rules, a DTF print will easily outlast the shirt itself. That said, I have seen cheap transfers from low-quality powder crack after a few washes. So do not skimp on consumables. Buy reputable film and powder. Your customers will notice the difference.
How to Get Started with DTF Without Breaking the Bank
If you are curious about DTF but not ready to buy a printer, you have options. Many companies sell pre-printed DTF transfers by the sheet. You can order a gang sheet with your designs, and all you need is a heat press. This is a fantastic way to test the waters. I started that way, ordering transfers from a supplier for about $0.50 per square inch. It let me fulfill small orders without any equipment investment. Once I saw the demand, I bought my own setup. If you go that route, here is a quick checklist:
- Choose a reputable transfer supplier. Ask for samples.
- Get a quality heat press with accurate temperature and pressure control.
- Practice on scrap shirts until you nail the application.
- Track your costs and compare to screen printing.
- Market your new capability to existing customers.
Also, consider the print-on-demand angle. If you run an online store, DTF allows you to offer a wider range of products without holding inventory. You can print transfers on demand and apply them to blanks as orders come in. That reduces waste and lets you test new designs with minimal risk.
Frequently Asked Questions About DTF Printing
Is DTF printing better than screen printing?
It depends on your order size and design. For small batches and full-color designs, DTF is faster and cheaper. For large runs of simple designs, screen printing is more cost-effective and offers a softer hand feel. Many shops use both.
Can I use DTF on 100% polyester?
Yes, DTF works great on polyester, including athletic wear and jerseys. The low-temperature application (around 300°F for 15 seconds) prevents dye migration, which is a common problem with screen printing on poly.
How do I wash a DTF-printed shirt?
Turn the shirt inside out, wash in cold water with mild detergent, and tumble dry low or hang dry. Avoid fabric softener and bleach. Do not iron directly on the print. Following these steps will keep the print looking new for years.
What is the minimum order for DTF?
There is no minimum. You can print one transfer or one shirt. That is the beauty of DTF. It is perfect for one-offs, samples, and personalized gifts.
Do I need a special printer for DTF?
You can convert certain Epson printers with DTF inks and a RIP software, or buy a dedicated DTF printer. If you are not ready for that, you can order pre-printed transfers from a supplier and just use a heat press.
At the end of the day, DTF is another tool in your toolbox. It is not a replacement for screen printing, but it fills a gap that many shops struggle with: small, complex orders that used to be money-losers. If you embrace it with realistic expectations, it can open up new revenue streams and make your customers happier. And that is what this business is all about.